Why the flux pot deserves engineering attention
In many galvanizing plants, the flux tank is the least instrumented vessel in the process, and one of the most influential. Poor flux management can contribute to four costly losses:
- Flux make-up: salts lost through carryover, drag-out, fume and waste removal.
- Zinc ash and dross: contaminants carried into the kettle increase material losses and clean-up.
- Rework: black or bare spots interrupt production and can require repair or rejection.
- Waste disposal: spent flux and iron-rich sludge carry treatment and disposal costs.
The flux bath is not simply a chemical dip between pickling and galvanizing. It is part of the plant’s thermal and chemical process chain. Its performance depends on rinse quality, work handling, dryer design, kettle operation and fume capture. Managing these interfaces is an extension of furnace and line engineering, and a practical route to better yield and profitability.
Benchmark caveat: All numerical figures in this article are indicative benchmarks drawn from published industry surveys and supplier or practical references. Actual operating values vary with plant design, line speed, workpiece surface area, steel chemistry, flux formulation and local permit conditions. Confirm setpoints through site trials, laboratory analysis and supplier guidance.
What the flux bath does, and why ACN matters
Zinc ammonium chloride (ZAC) pre-flux protects cleaned steel from oxidation between rinsing and immersion. It helps maintain a chemically active surface, supports zinc wetting and contributes to an even coating. It is a barrier against re-oxidation, not a substitute for effective pickling, rinsing or drying.
Flux selection is often described using ACN (Ammonium Chloride Number), the NH₄Cl/ZnCl₂ ratio. Formulation should match the dryer temperature, steel section and handling system, not just the price per kilogram.
| Flux family | Indicative ACN | Typical process fit |
|---|---|---|
| Double salt | ~0.8 | More thermally stable; often preferred where steel is preheated or dried at higher temperature |
| Triple salt | ~1.17 | More active; common on lines without preheaters or with simpler dryers |
| Higher-ACN “quadraflux” | ~1.6 | Used in some pipe applications for thinner coatings where transport equipment supports the process |
The AGA’s 2019 process survey found pre-flux was used by 96% of respondents; triple salt was the most commonly reported mixture. These are survey results, not universal specifications. Changing ACN without checking coating quality, drying and fume behaviour can trade one process problem for another.
Four control parameters for bath stability
Establish a site-specific operating window and record results consistently. Density alone is not a chemistry test: it changes with salt concentration and dissolved iron, so use it alongside pH and iron analysis.
| Parameter | Typical target or practice | Action limit / trigger | Consequence of drift |
|---|---|---|---|
| Total concentration | 200–700 g/L; many lines operate at 300–500 g/L | Outside the plant’s validated band | Too low can impair activity; excess can raise carryover and fume |
| pH | 4.0–4.5; some practices accept up to 5.5 | Investigate below ~3.5; correct based on measured samples | Low pH increases soluble iron and corrosion; high pH can affect flux performance and drying |
| Dissolved iron | Keep below ~2 g/L where practicable | Action around 4 g/L; published guidance also cites under ~1 wt% or 5 g/L | Higher iron loading is associated with dross, ash and unstable flux performance |
| Bath temperature | Commonly 50–70°C | Compare with the chosen flux supplier’s operating range | Changes activity, drainage and drying behaviour |
| Specific gravity / °Baumé | AGA survey average ~15.4° Baumé; many plants reported ~13° | Trend against the plant’s own validated baseline | Density can mislead if iron and salt concentration are not also checked |
| ACN / salt balance | Select for flux type and process conditions | Recheck after major make-up or chemistry changes | Poor match to dryer and steel section can affect activity and coating results |
Use ammonium hydroxide to raise pH and hydrochloric acid to lower it; make measured, gradual corrections with adequate mixing and re-testing. The AGA pH guidance recommends a 4.0–4.5 pH range for heated pre-flux and cautions that plant readings may need laboratory verification. Avoid estimating chemical additions: the bath’s buffering capacity matters.
Published cost references are useful only when normalised by output. Practical industry data put flux consumption at roughly 0.5 kg per 100 kg of zinc consumed where the bath is run without purification, while other guidance cites around 1.2 kg of flux per tonne of galvanized steel; the spread reflects surface area and work mix rather than efficiency alone. Zinc ash generation commonly sits in the region of 2–5 kg per tonne of steel treated. Both numbers are reference points for a plant's own trend line, not targets to be copied from a catalogue.
Upstream discipline: prevent contamination before it reaches the tank
The cheapest flux control often happens before the flux tank. Residual pickling acid and iron salts carried on the work can consume bath capacity and add contamination. Two-stage static rinsing, spray rinsing or agitation can reduce this carryover. The AGA guidance also emphasizes good rinsing to reduce the frequency of pH adjustments.
Control the physical movement of work as carefully as the bath:
- Allow consistent drainage after pickling and rinsing; avoid transferring trapped liquid.
- Review jig orientation and spacing so parts drain rather than retain acid or flux.
- Keep rinse water quality and overflow or replenishment practices under review.
- Dry fluxed work at around 100–120°C, and avoid exceeding about 150°C unless the flux supplier has validated the conditions.
- Confirm dryer dwell time and temperature uniformity across the load, not just the control-panel setpoint.
Wet steel entering zinc at roughly 445–460°C is a classic contributor to black or bare spots and can produce a sudden, hazardous fume event. Water carryover can also cause violent spattering. The UK process guidance describes instant fume at immersion and identifies drying as a way to minimize water carryover.
Daily operator checks
- Record bath temperature, pH and density using a consistent sampling method.
- Check for visible settling, unusual colour or solids, and confirm circulation or agitation.
- Inspect rinse performance, work drainage and dryer temperature indication.
- Look for flux drag-out, leaks and signs of corrosion around the tank and pipework.
- Confirm fume extraction is operating before dipping and note any escape from the capture zone.
Iron: the slow poison
Iron enters the flux principally through pickling-acid carryover and iron salts left on insufficiently rinsed work. If the flux tank becomes the plant’s settling tank for pickling by-products, dissolved iron builds up and contaminant solids can be transported toward the kettle. High iron loading is associated with more dross and ash, poor drying and increased coating defects.
The pH is a key iron-solubility lever: below about pH 3.5, iron solubility rises sharply. This is why operators should treat a declining pH as an early warning, not just a number to correct after coating problems appear. In addition to the AGA guidance, record iron measurements over time; a single density or visual check cannot show whether the bath is accumulating metal.

Flux regeneration: remove iron, retain useful liquor
A common regeneration approach is a side-stream oxidation–precipitation–filtration loop:
- Draw flux from the operating tank into a reaction vessel.
- Dose hydrogen peroxide to oxidize ferrous iron (Fe²⁺) to ferric iron (Fe³⁺).
- Add ammonia under controlled conditions to bring pH to approximately 4–5, encouraging iron hydroxide precipitation.
- Separate the precipitate by settling and filter press.
- Return clarified flux to the tank, then verify its chemistry before normal operation.
PLC control can coordinate pH, density and iron measurement with reagent dosing, pump operation and safety alarms. Instrumentation does not eliminate laboratory checks; it helps operators act consistently and early.
Reported supplier outcomes include roughly 50–60% lower waste-disposal volume, along with reduced dross and zinc consumption, lower chemical use and longer bath life. These are reported results, not guaranteed savings. Validate them with a site mass balance that accounts for salt additions, flux losses, sludge, zinc ash and dross. Regeneration is not zero-waste: iron hydroxide sludge remains a disposal stream, and its classification and disposal route should be confirmed locally.
Before purchasing a system, ask for:
- A trial or mass-balance demonstration using representative plant liquor.
- Sludge analysis, moisture content and a realistic disposal estimate.
- Reagent consumption per volume of liquor treated and per kilogram of iron removed.
- Expected performance across the plant’s pH and iron range, including buffer capacity.
- Instrument calibration, maintenance, operator training and spares requirements.

Treatment options compared
| Approach | Iron control | Flux yield | Waste volume | Operator dependency | Footprint and complexity | Best suited to |
|---|---|---|---|---|---|---|
| Manual dump-and-remake | Reset by replacement, not continuous control | Low; usable salts leave with spent bath | High | High | Low equipment complexity | Small or intermittent operations |
| Decant-and-settle | Limited; depends on settling and pH | Moderate, with uncertain recovery | Moderate | High | Low to moderate | Low-throughput plants with manageable iron loading |
| Batch chemical treatment | Periodic removal through reaction and filtration | Moderate to high if dosing is controlled | Reduced, but sludge remains | Moderate to high | Moderate | Plants able to schedule treatment and verify chemistry |
| Continuous automated regeneration | Ongoing monitored removal | Potentially highest, subject to process validation | Can be substantially reduced | Lower routine dosing burden; skilled oversight still needed | Highest | High-throughput or cost-sensitive lines with measurable iron loading |
Why this is furnace and line engineering, not just chemistry
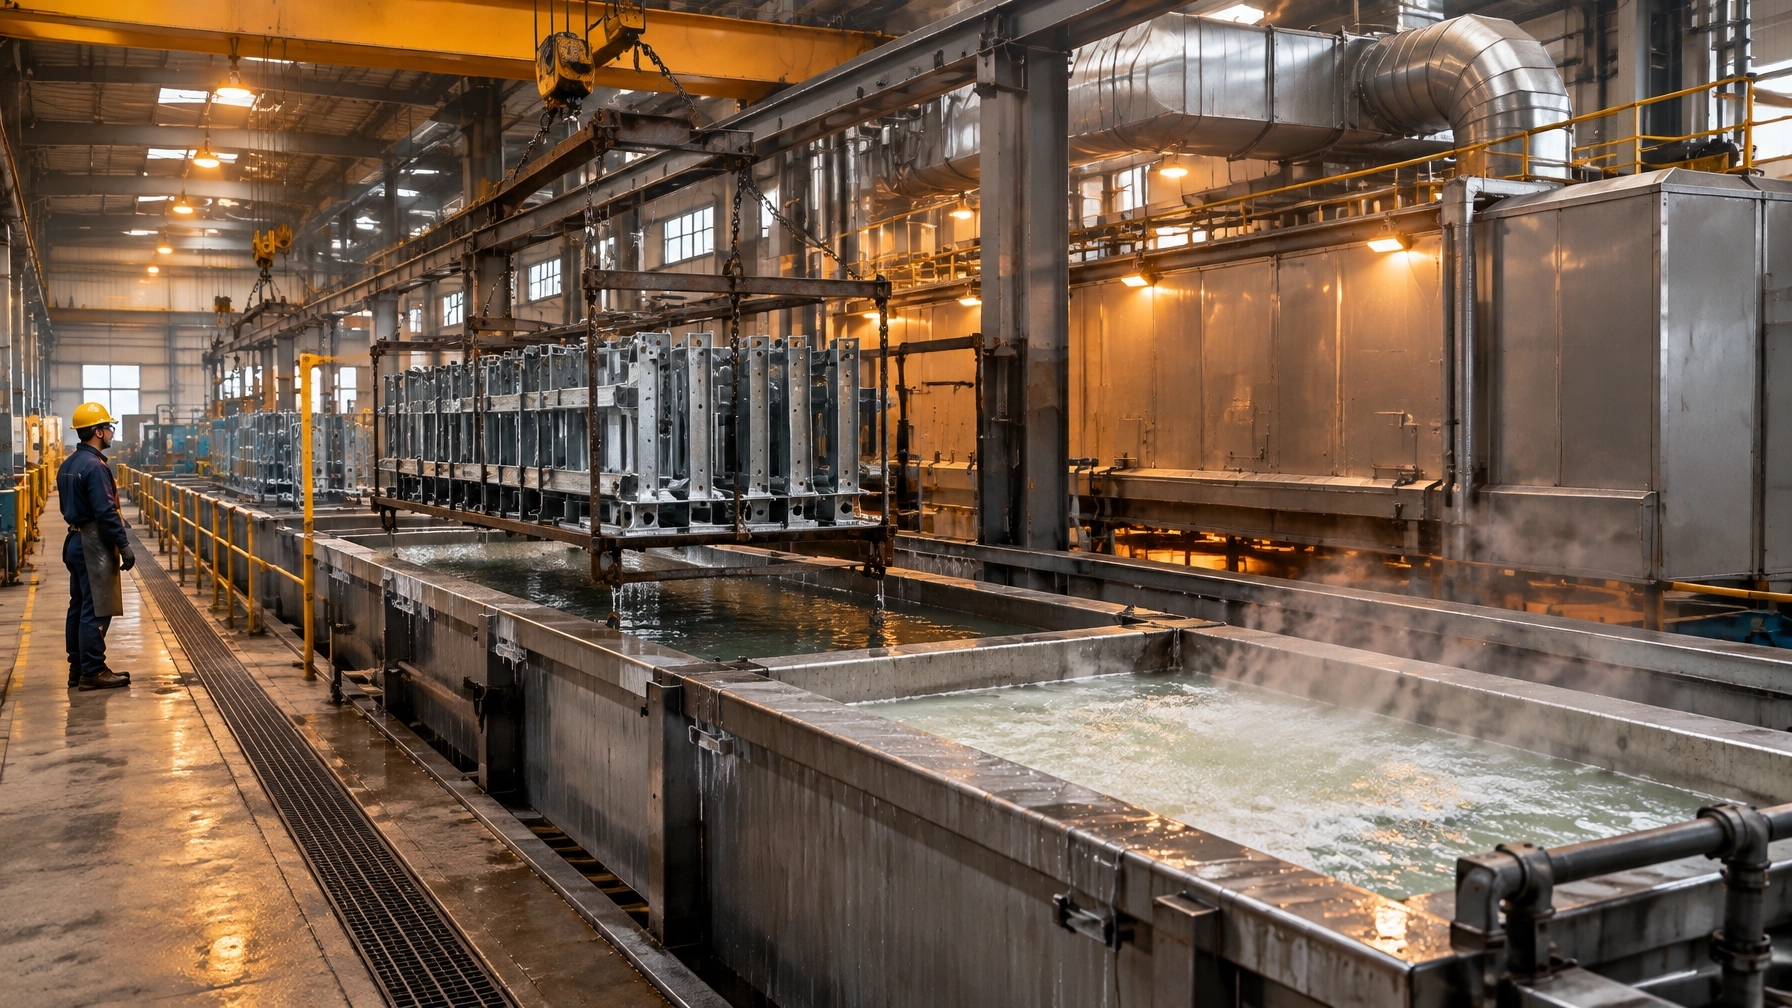
The bath cannot be optimized in isolation. Dryer temperature uniformity and dwell affect flux stability and the condition of the work at the kettle. Tank heating and materials must be appropriate for the chemistry. Tank sizing should account for work volume and drag-out. Fume hoods, ducting and arrestment must capture emissions at source without obstructing safe handling. Corrosion protection and planned maintenance help prevent leakage and unplanned downtime.
The UK process guidance lists an HCl emission limit of around 30 mg/m³ for hydrochloric-acid pickling, while its galvanizing-bath provisions address particulate emissions separately. That HCl figure is not a universal flux-fume stack limit; confirm applicable limits, monitoring and consent conditions with the local regulator. The guidance also describes enclosure and extraction as key controls for kettle fume.
It is worth saying plainly that escaping fume is escaping salt. Every kilogram of ammonium chloride that leaves through the arrestment or the roof vent was bought, paid for, and never did any work on the steel. Extraction performance belongs in the consumable-cost review alongside the compliance file, and hood geometry, capture distance, duct velocity and filter condition deserve the same engineering attention as burner tuning on any other furnace in the plant.
Continental Furnaces integrates kettles, dryers, preheat and fume hoods as part of engineered hot dip galvanizing plant solutions. Upstream pickling plant design is equally relevant: rinse performance is a direct input to flux quality.
2026 technology and market updates
- Inline density, pH and iron analysers are increasingly paired with closed-loop reagent dosing. Instruments still require calibration and periodic laboratory confirmation.
- Digital flux KPIs, including kilograms of make-up flux per tonne of steel and measured flux deposition in g/m², can reveal losses earlier than monthly purchasing totals. Establish deposition targets through plant trials; published practical data show flux usage can vary with temperature and dwell.
- Predictive maintenance for pumps, filters and exhaust fans can be linked to furnace spare parts planning, reducing downtime risk.
- Low-fume and higher-stability formulations are options to evaluate against the specific steel mix, dryer and coating requirements.
- Tighter HCl and particulate consents are increasing attention on enclosed dipping, extraction design and arrestment performance.
- Water and effluent pressures strengthen the business case for reducing carryover and evaluating closed-loop regeneration.
Four-phase implementation roadmap
Phase 1: Baseline and mass-balance audit
Measure flux make-up, bath volume, density, pH, iron, ash, dross, sludge and reject rates. Normalize data by production and, where feasible, surface area.
Phase 2: Rinse and chemistry discipline, no capex first
Improve rinse staging, agitation, drainage and sampling. Set written limits, correction procedures and operator responsibilities before buying regeneration equipment.
Phase 3: Evaluate and install regeneration and fume capture
Compare treatment options using actual plant liquor and operating data. Review extraction coverage, duct condition, arrestment and permit requirements as a connected system.
Phase 4: Sustain performance
Train operators, review trends, calibrate instruments and keep critical spares available. Use monthly performance reviews to adjust process limits as the product mix changes.
KPIs to put on the board
Track the measures that connect bath chemistry to cost, quality and compliance:
- kg flux per tonne of steel
- g/m² flux deposition, established for the plant’s product mix
- Iron concentration, g/L, with trend and action limit
- Percentage of readings within the pH control band
- Black-spot reject and rework rate
- Zinc ash, kg/t, and dross generation, read alongside the kettle and zinc-yield picture
- Sludge, kg/t, plus disposal cost
- HCl and particulate results at the relevant stack, against local consent
A process discipline that travels across industries
The same principles apply in the wire and cable industry, where continuous lines combine surface preparation, rinsing, fluxing, drying and coating. They also matter to fabrication shops serving a steel rolling mill, and to manufacturers running coating lines alongside other thermal processes. Buyers of heat treatment furnaces, an aluminum melting furnace or a melting furnace for steel may also benefit from seeing coating chemistry and heat transfer as one connected production system.
As an industrial furnace manufacturer, Continental Furnaces supplies thermal processing equipment and industrial furnace systems, as well as galvanizing plants, metal recycling furnace solutions and furnace spare parts. Our engineering experience spans different metals, line configurations and production demands; our heat treatment furnaces are one part of that wider capability.
Build the next improvement into an enduring partnership
A flux-control project is most effective when it starts with plant data and continues through equipment selection, commissioning and operator support. Bring your current bath readings, production profile, reject data and waste costs to a technical discussion with Continental Furnaces. Together, we can identify the right next step for quality, efficiency and sustained competitive advantage.
Request a consultation and begin an enduring partnership: Contact Continental Furnaces.