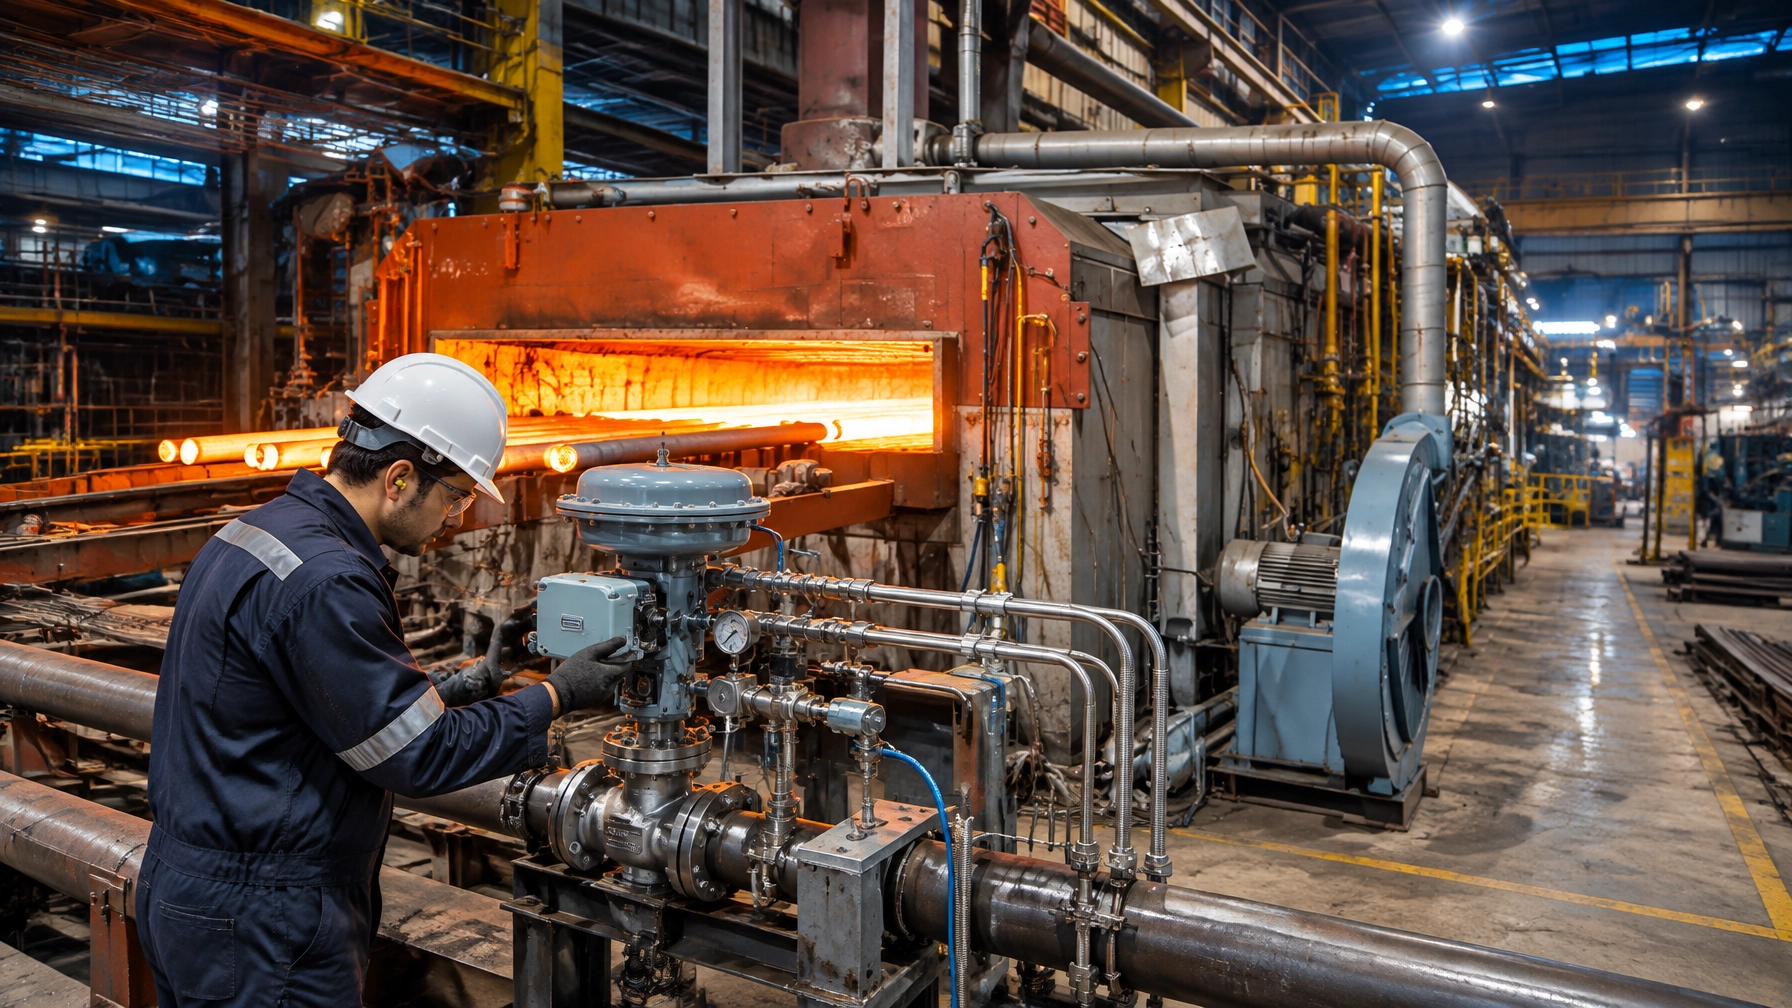
Every furnace trip that ends with a fuel safety shutoff valve closing has a cause upstream of that valve, and in a large share of cases the cause is the air. Instrument air is among the cheapest utilities per cubic metre and among the most expensive per failure, because the failure is not simply a utility bill: it is a stopped furnace. A gas-fired furnace cannot keep operating safely without air to move its controls. Its safety shutoff valve is spring-return and normally closed by design, so plant protection and production depend on the same 6 mm tube. The compressor is rarely the whole reliability problem. Air treatment and distribution downstream of it are where moisture, contamination, pressure loss and leakage undermine the system.
This is not the 14 November post on combustion air and flue-gas fans, which covered the air burned, ductwork, dampers, VFDs and fan vibration. It is not the 6 November post on burner management logic, which covered interlock architecture, purge and flame-failure logic. This post concerns instrument air that moves valves, and the evidence required to prove that the valves actually moved. It is also distinct from the 15 November emissions monitoring post and the 17 November carbon intensity post.
Caveat: The technical content is a reading of published standards and general industry guidance. It is not a substitute for OEM instructions, the requirements of the authority having jurisdiction, or a site-specific safety review.
The utility that nobody owns
Instrument air often sits between departments. The utility engineer installs the compressor and dryer; the instrument technician maintains the devices; the furnace OEM specifies the actuators and valves; and nobody clearly owns the performance of the complete system. That gap is one reason leaks amounting to 20 to 30 percent of compressor output can persist, and a dryer that has quietly lost its dew point may be discovered on the coldest morning rather than at the next inspection.
The consequences cross maintenance, safety and production boundaries:
- Wet air corrodes internals, blocks small passages and can freeze in exposed tubing.
- Oil and particulates contaminate solenoids, positioners and actuator seals.
- Pressure loss can prevent a valve from completing its required stroke.
- Poorly adjusted actuators may be blamed on air supply when the actual fault is mechanical.
- A trip can expose refractory and shell to abrupt thermal change, adding damage to lost production.
A furnace needs air that meets its actual quality requirement at the device, not simply a compressor that appears healthy at its discharge.
What the two standards actually specify
ISA-7.0.01 sets instrument-air quality requirements. ISO 8573-1:2010 classifies compressed-air purity using three separate class numbers: particles, water, oil. It is not one overall purity rating.
| Topic | ISA-7.0.01 | ISO 8573-1:2010 | What the furnace actually needs |
|---|---|---|---|
| Dew-point basis | At least 10°C below the minimum ambient temperature to which any part of the system is exposed, and never above 4°C at line pressure | A fixed water-class number: class 1 at −70°C or better; class 2 at −40°C or better; class 3 at −20°C or better; class 4 at +3°C or better | A target based on the plant’s coldest seasonal exposure and the route to each actuator |
| Particle limit | Maximum particle size 40 micrometres | Classes 1, 2 and 3 set particle counts by size band; see the limits below | Filtration suited to the smallest passages and the device maker’s requirement |
| Oil limit | Total liquid, aerosol and vapour oil not more than 1 ppm by weight or volume | Class 1: 0.01 mg/m³ or less; class 2: 0.1 or less; class 3: 1 or less | A declared class backed by measurement and suitable filtration |
| Designation | A quality standard, not a single purity number | Always three class numbers: particles:water:oil | Specify all three classes, then verify the air at relevant points |
| Practical reading | Dew point depends on minimum ambient exposure | A class states a fixed purity limit | Choose a specification that remains fit for seasonal exposure and device duty |
For ISO particle classes, the permitted counts per cubic metre in the 0.1 to 0.5, 0.5 to 1.0, and 1 to 5 micrometre bands are respectively: class 1, 20,000 / 400 / 10; class 2, 400,000 / 6,000 / 100; class 3, no count specified in the smallest band, then 90,000 / 1,000. Class 0 is not a universal purity level. It is a class defined by the user and guaranteed by the supplier.
A commonly specified grade for valve positioners and pneumatic instruments is 1.4.1: particle class 1, water class 4, oil class 1. It is a wet specification. It can be adequate for an instrument in a conditioned panel, but it is not automatically adequate for an actuator exposed on a furnace roof in winter.
The dew point is a seasonal number and not a fixed one
ISA-7.0.01 ties the required pressure dew point to the minimum ambient temperature anywhere the system is exposed. It does not prescribe one universal dew-point target for all climates. The same installation can meet the requirement in Chennai and fail it in a north Indian winter if exposed lines, drains or actuator connections see colder conditions.
A refrigerated dryer typically delivers a pressure dew point of about +3°C to +4°C. Any downstream line passing through a space colder than about +3°C can condense moisture. A pocket that drops below zero can freeze. The freeze may remain unnoticed until an actuator is asked to move, precisely when the control system needs a reliable response.
Desiccant drying can reach −40°C or better, but the dryer outlet alone is not the whole assessment. Trace the route to the device, identify outdoor and unheated sections, and check low points where condensate can collect. Continuous dew-point monitoring at the dryer outlet, with an alarm in the control room, is stronger evidence than a local gauge that nobody reads.
The dryer is a compressor load with a purge valve
Dryer selection is an energy and reliability decision. A dryer that removes water may use compressed air to do so. Heatless regenerative desiccant dryers commonly consume 15 to 25 percent of rated flow as purge, with a typical order of magnitude around 15 percent. That is already-dried air vented to atmosphere, which the compressor must continually replace. Buying a dryer on capital cost alone makes an energy decision by accident.
| Architecture | Pressure dew point achieved | Regeneration or purge cost | Where it belongs in a furnace plant | Failure signature when it degrades |
|---|---|---|---|---|
| Refrigerated | Roughly +3°C to +4°C | No desiccant purge; compressor and dryer energy still apply | General plant air where the seasonal exposure permits this dew point | Rising outlet dew point, condensate downstream, or excessive pressure drop |
| Heatless desiccant | −40°C or better | Purge commonly 15% to 25% of rated flow | Cold or exposed routes requiring a low dew point | Dew point rises as desiccant or switching performance degrades |
| Heat-of-compression desiccant | Desiccant drying; confirm the guaranteed dew point for the offered design | Uses available compressor heat; confirm purge and auxiliary energy with the supplier | Sites able to use compressor heat and needing desiccant-grade air | Outlet dew point drifts from the guaranteed value or switching faults appear |
| Point-of-use desiccant | Set by the selected unit and its verified duty | Local regeneration or purge burden; check the device specification | A cold, remote actuator branch where central drying alone is insufficient | Local moisture breakthrough or falling pressure at the device |
A pressure drop greater than about 5 psi across a dryer indicates a potential failure. Include pressure measurements across dryers and filters in routine checks, and compare dew point with the system’s seasonal requirement, not just the dryer’s nameplate.

Leaks are a permanent process load nobody scheduled
Well-maintained systems lose about 10 percent of compressor output to leaks; a common benchmark is to keep leakage below 10 percent. Poorly maintained systems commonly reach 20 to 30 percent. The energy calculation makes the scale plain. At a specific power of about 18 kW per 100 cfm, one cfm running continuously uses 0.18 kW × 8,760 hours, or about 1,577 kWh per year. A quarter-inch orifice at roughly 100 psig passes about 104 cfm. That represents around 164,000 kWh per year, before any tariff is applied. Multiply by your own tariff to assess the cost.
A two-hour receiver bleed-down test is an accessible Sunday exercise for a shift team. Isolate production demand as the site procedure allows, record system pressure, bleed down and time the pressure fall. Estimate leakage as:
Leakage in cfm = total system volume (ft³) × pressure drop (psi) ÷ [test time (minutes) × 14.7] × 1.25
The 1.25 factor accounts for the fact that leak rate falls as pressure falls. Total system volume means receivers plus mains plus piping, not just the receiver. The result is an estimate; use appropriate site controls and a qualified review where required.
Leak repair alone does not guarantee savings. Part-load is where compressed-air economics collapse. A machine rated at 21.3 kW per 100 cfm at full load can rise to roughly 44 kW per 100 cfm at 40 percent load under modulation control. Fixing leaks and then throttling the same compressor can mean fewer cfm at worse specific power. Sequencing and storage, not leak repair alone, capture the efficiency gain.
Header pressure is another common trap. A widely used guideline is that reducing system header pressure by 2 psi corresponds to roughly 1 percent saving in total energy. Raising pressure to compensate for one marginal actuator or a long restrictive run imposes a permanent energy cost for what may be a local mechanical or distribution fault.
Storage stabilises the header during sudden demand. Historical practice used 1 gallon per cfm; current practice commonly uses 3 to 5 gallons per cfm of trim compressor capacity, and 2 to 4 gallons per cfm for variable-speed machines. Storage helps keep header pressure above the trip point during a large actuator demand. It is one of the least complicated reliability investments in the system.

A positioner that never stops breathing
Positioner steady-state air use typically spans 0.035 to 0.71 scfm, depending on model, design and supply pressure. Bleed rises with supply pressure. For a practical sizing and auditing example, 200 positioners at 0.3 scfm each consume 60 scfm continuously. That is a persistent load which no production cycle explains. Check every device against its own datasheet; the range is not a substitute for model-specific data.
Audit continuous bleed before increasing compressor capacity or header pressure. Confirm the positioner is correctly sized, supplied at its specified pressure, and not compensating for a sticking valve or a poor linkage.
The actuator is a spring and the air only holds it back
A spring-return actuator moves the valve to its fail-safe position by spring force when air or power is lost. Bench set is the spring preload established with the actuator disconnected from the valve. Once installed, that preload must overcome packing friction, static unbalance and process forces to seat the valve.
When a valve will not close tightly despite ample supply pressure, investigate the mechanics before blaming air. Common causes include insufficient bench set, the wrong spring rate, incorrect rated travel or a linkage error. Raising supply pressure to force closure trades a mechanical fault for a permanent energy cost and can over-stroke the actuator.

Partial stroke testing is evidence of movement and not of tightness
Under the NFPA 86 framework, safety shutoff valves are normally closed and automatically shut off fuel on abnormal conditions and shutdown. A valve proving system checks closure by detecting leakage. A proof-of-closure switch activates only after the valve is fully closed. Where combustion air is mechanically supplied, airflow or pressure must be proven and interlocked so fuel cannot be admitted before combustion air is established, and fuel is shut off on combustion-air failure.
The critical distinction is that installing a proving system does not replace required seat leakage testing. Seat leakage testing of safety shutoff valves and valve proving systems is required at least annually under the applicable framework.
Partial stroke testing moves a valve through a defined portion of travel to demonstrate that it is not stuck. Diagnostic instruments can record response time and pressure. Common diagnostic-coverage assumptions for safety-integrity credit are 60 to 70 percent, with 70 percent used for severe or dirty service and 60 percent for very clean service. Coverage above about 85 percent is difficult to substantiate in process applications. The decisive limitation remains: partial stroke testing is evidence of movement, not seat tightness. A valve can move freely and still leak through a damaged seat.
Solenoid-operated valve data, including NUREG/CR-4819 and related operating experience, identify failure to operate as the dominant mode. Worn or degraded parts and foreign-material contamination lead, followed by coil short and coil open. Moisture and contamination therefore point back to filtration and dew point, not simply to keeping spare solenoids on a shelf.
Tubing fittings and the three failures you will find
Start inspection at the exposed ends of the system. A cracked nylon line on a furnace roof is not just a leak; it is a latent trip. Nylon is vulnerable to ultraviolet degradation and embrittlement, so it is generally discouraged for permanent outdoor or safety-critical service.
Material choice should match the environment:
- Stainless steel is preferred in harsh conditions. 316L is common; 6Mo or super duplex may be appropriate where chloride is aggressive.
- Copper is common indoors, but vibration and heat can make it work-harden and embrittle.
- Nylon should be assessed carefully where UV, heat or safety-critical service is present.
Three findings account for most of what a survey turns up, and only one of them is solved by ordering a part:
- Moisture and contamination. Damp air or oil carry-over attacks solenoids, positioners and seals, and the damage shows up as a sticky valve rather than as a wet line.
- Pressure loss. Leaks and restrictions starve the actuator of the flow it needs during a stroke, which is invisible while the valve is sitting still.
- Mechanical faults misread as weak supply. A valve that will not seat is usually a bench-set, spring or linkage problem, and the instinct to raise header pressure hides it.
Solenoid failure data reinforces the first point: foreign material and degradation matter more than coil failure. A complete field inspection checks material, fittings, support, vibration, drain points, filter condition and actual actuator response.
Where this lands across furnace applications
A steel rolling mill needs dependable furnace-side actuation through repeated production demand, because a mill that stops for a valve is a mill that stops for a shift. Heat treatment furnaces rely on controlled cycles and protected shutdowns, and their atmosphere and quench sequences are the least tolerant of an unplanned interruption. An aluminum melting furnace concentrates heat, moisture and exposed tubing in the same small area, which is an air-quality problem disguised as a refractory problem, while a melting furnace for steel cannot treat air quality as a peripheral utility issue at all. Across thermal processing equipment, the air system has to match the device and the climate rather than the datasheet. A hot dip galvanizing plant carries outdoor exposure and chloride into its distribution in a way an indoor shop never does, and a metal recycling furnace benefits most when utilities, safety and maintenance share a single named owner. For the wire and cable industry, line availability and predictable furnace control are the whole operational requirement. An industrial furnace manufacturer should make interface requirements explicit at the order stage, while operators of industrial furnace systems must verify installed air quality and valve evidence rather than assume them. Planned furnace spare parts support recovery, but measurement and correct installation prevent the failure in the first place.
Keep the air side stocked against the trip you can prevent
Stock components in the material, size, voltage and rating actually installed, and verify compatibility against OEM documentation. Useful items include:
- Filter elements and coalescing elements in installed sizes, plus the desiccant charge.
- A dew-point sensor and its calibration reference.
- Solenoid coils and complete solenoid valve assemblies in plant-standard voltages.
- Spring-return actuator spring sets and diaphragm or piston seal kits.
- A positioner and its I/P converter module.
- Proof-of-closure switch assemblies.
- Valve seat and plug kits for each furnace’s safety shutoff valves.
- Tubing in the installed material and diameter, with a full set of fittings and push-fit cartridges.
- A spare pressure regulator per header, and pressure gauges with the correct range.
- A portable dew-point meter for field checks.
The most expensive spare is the correct part discovered to be in the wrong material grade during a shutdown. Keep the specification and material traceability with the stock, not only in a purchasing record. See available furnace components and accessories.
From utility to instrument: a five-phase instrument air programme
Phase 1: Boundary and ownership
Name an owner. Draw the system from compressor discharge to the last actuator, including dryers, filters, receivers, headers, branches and exposed lines. Mark where responsibility changes hands. Without a named owner and boundary map, the utility remains easy to neglect.
Phase 2: Measurement
Install dew-point monitoring at the dryer outlet and alarm it to the control room. Log pressure drop across each dryer and filter, trend header pressure, and run the receiver bleed-down test monthly. Record the test conditions and include all connected system volume in the leakage estimate.
Phase 3: Drying and distribution correction
Close the gap between measured dew point and the coldest seasonal exposure. Add point-of-use drying where lines run cold. Replace degraded tubing and correct fittings or support problems. For valves that will not seat, verify bench set, spring selection, travel and linkage before changing air pressure.
Phase 4: Demand reduction
Run a leak survey and reduce leakage below 10 percent. Audit positioner bleed, set header pressure to the requirement rather than the worst local fault, and size storage for demand transients. Sequence compressors on flow rather than simply holding pressure with an inefficient part-load machine.
Phase 5: Evidence and assurance
Maintain annual seat leakage testing in line with the applicable standard and OEM instructions. Keep valve proving records and partial stroke test records, clearly stating what each test proves and what it does not. Maintain a trip-cause register that distinguishes an air-caused trip from a valve-caused trip. The two are routinely conflated, and that distinction changes who fixes it. Separate the evidence so maintenance addresses the actual failure mechanism and the safety record remains defensible.
Build an enduring reliability partnership
A dependable furnace depends on more than a compressor specification. Dew-point architecture, leak control, storage, actuator mechanics and documented proof testing work together to protect uptime, energy performance and safe operation. Continental Furnaces brings 35 plus years of furnace expertise, ISO-certified quality and prompt service to support thermal processing requirements and lifecycle reliability.
Request a consultation to review your furnace application, utility boundary and instrument-air requirements. Make the discussion a strategic step toward sustained competitive advantage through an inquiry to Continental Furnaces.
References
- ISA-7.0.01, Quality Standard for Instrument Air.
- ISO 8573-1:2010, Compressed air, contaminants and purity classes.
- NFPA 86, Standard for Ovens and Furnaces.
- U.S. Department of Energy, Improving Compressed Air System Performance, A Sourcebook for Industry.
- U.S. Department of Energy, Compressed Air Tip Sheet 3, Minimize Compressed Air Leaks.
- Compressed Air Challenge, Fact Sheet 7, Compressed Air System Leaks.
- NUREG/CR-4819, Aging and Service Wear of Solenoid-Operated Valves.
- IEC 61511, functional safety and partial stroke test coverage guidance.
- ISO 8573-2 and ISO 8573-3, oil aerosol and humidity measurement methods.