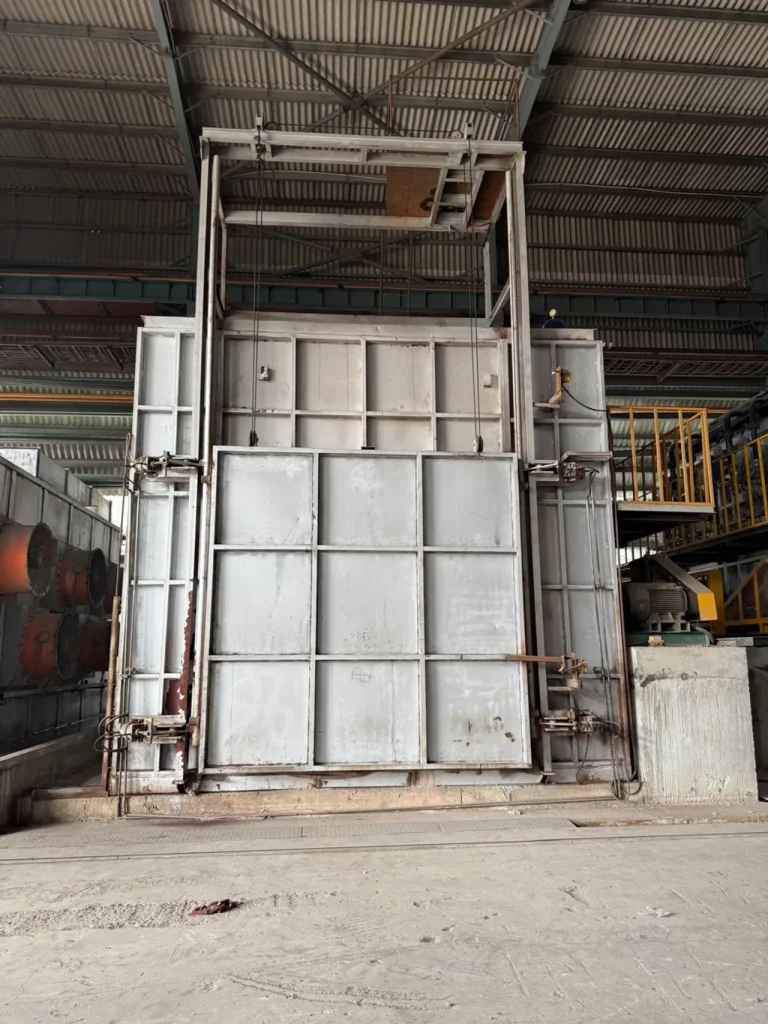
The 2026 decarbonization agenda has moved beyond long-term ambition. For every steel rolling mill, melting shop, and downstream metal processor, fuel selection now affects production cost, export competitiveness, carbon reporting, and access to international markets.
The European Union’s Carbon Border Adjustment Mechanism (CBAM) entered its definitive regime on 1 January 2026. Iron, steel, aluminium, hydrogen, electricity, cement, and fertiliser imports are covered. This makes furnace-level carbon intensity a commercial performance indicator, not merely an environmental metric.
Typical legacy gas-fired reheating furnaces operate around 0.082–0.095 tCO₂ per tonne of steel, while optimized high-efficiency systems can reach approximately 0.068–0.073 tCO₂ per tonne under suitable operating conditions. These are planning benchmarks, not universal guarantees, but they demonstrate the value of fuel switching and combustion modernization.
The 2026 fuel-switching decision
Plant managers are now evaluating four connected pathways:
- Hydrogen-ready combustion using natural gas today and hydrogen blends later
- Direct electric reheating or melting where grid capacity and tariffs permit
- Hybrid gas-electric systems that separate high-temperature heating duties
- Oxy-fuel and regenerative burner upgrades as transitional carbon-reduction measures
The correct answer depends on production temperature, throughput, steel grade, available utilities, regional carbon intensity, and the plant’s required return on capital.
The strategic objective is not to replace one fuel blindly. It is to create a flexible thermal platform that can operate safely and profitably through several energy-market scenarios.
Hydrogen-ready burners: readiness is an engineered system
Hydrogen-ready equipment is not defined by a burner label alone. It requires coordinated design across the complete gas train, furnace chamber, controls, safety systems, and refractory package.
A hydrogen-ready furnace should address:
- Gas-train capacity for changing fuel volume and pressure
- Burner turndown across natural gas and hydrogen-blend operation
- Flame detection, ignition, purge, and emergency-shutdown logic
- Flame speed and heat-flux changes at hydrogen concentrations
- NOₓ monitoring and mitigation
- Furnace-pressure stability
- Refractory exposure to altered flame patterns
- Oxygen-trim and combustion-control compatibility
- Safe ventilation, leak detection, and hydrogen-rated components
Hydrogen has a higher flame speed and lower volumetric energy density than natural gas. As a result, the same thermal duty can require significantly greater fuel volume. Burner ports, valves, piping, control algorithms, and safety interlocks must be sized for the intended blend range.
A practical sequence is:
- Natural gas operation with hydrogen-ready hardware
- 5–20% hydrogen blending during a controlled pilot
- 30–50% blending after combustion and quality validation
- Higher blends or 100% hydrogen only after full engineering approval
The furnace must maintain temperature uniformity, material quality, throughput, and emissions compliance at every stage.
Electric reheating and melting: high efficiency, high infrastructure demand
Electric heating removes direct combustion emissions at the furnace, although total carbon intensity depends on the electricity source. Modern induction systems can achieve electrical efficiencies of up to 90%, according to published rolling-mill decarbonization research.
Electric systems are particularly relevant for:
- Billet, bloom, and bar reheating
- Electric melting of ferrous and non-ferrous metals
- Aluminium and copper processing
- Scrap-based metal recycling
- Booster heating before or after a gas-fired zone
- New production lines where electrical infrastructure can be designed from the outset
The main constraint is often not furnace technology. It is the grid.
Before approving an electric conversion, the plant must verify:
- Available connection capacity in MVA
- Transformer and substation requirements
- Electricity tariff structure and demand charges
- Power-quality and harmonic-control requirements
- Backup strategy during grid interruptions
- Renewable electricity availability
- Production impact during electrical-infrastructure construction
Electric reheating can deliver precise temperature control and rapid response, but a high-capacity installation may require substantial grid reinforcement. The business case must therefore include both furnace capital cost and electrical infrastructure.

Oxy-fuel and regenerative systems as transition technologies
Oxy-fuel and regenerative burners remain valuable when a plant needs measurable carbon reduction before hydrogen or electrical infrastructure becomes commercially available.
Indicative outcomes for suitable reheating applications include:
- 10–25% lower fuel consumption through improved combustion-air preheating or reduced exhaust volume
- Lower flue-gas volume with oxy-fuel combustion
- Faster heat transfer and increased furnace productivity
- Reduced dependence on conventional combustion air
- Compatibility with staged hydrogen conversion when correctly specified
These systems require careful control of oxygen supply, flame temperature, NOₓ formation, refractory loading, and furnace pressure. They are not automatic decarbonization solutions. Their value comes from acting as bridge infrastructure that lowers current fuel consumption while preparing the furnace for future fuel flexibility.
Conventional versus low-carbon furnace technology
| Technology pathway | Direct carbon profile | Typical efficiency or benchmark | Capital profile | Principal constraint |
|---|---|---|---|---|
| Legacy natural-gas furnace | Approximately 0.082–0.095 tCO₂/t steel | Baseline | Low sunk cost | Gas-price and CBAM exposure |
| Optimized gas furnace with advanced burners | Approximately 15–30% below legacy fuel use | Around 0.068–0.073 tCO₂/t in suitable cases | Moderate | Still dependent on fossil gas |
| Hydrogen-ready furnace operating on gas | Similar near-term carbon to gas system | Designed for staged 5–50% blending | Moderate, typically 10–20% above a standard burner package | Hydrogen supply and safety validation |
| Green-hydrogen combustion | Near-zero direct fossil CO₂ | Thermal efficiency remains process-dependent | High operating-cost exposure | Hydrogen price, availability, NOₓ, storage |
| Direct electric reheating or melting | Zero direct Scope 1 combustion emissions | Electrical efficiency up to approximately 90% for suitable induction systems | High, including grid upgrades | Capacity, tariffs, power quality |
| Gas-electric hybrid architecture | Reduced gas use with flexible dispatch | Dependent on operating strategy | Moderate to high | Control integration and load balancing |
Hydrogen-based reheating can cost 2.5–2.9 times current business-as-usual reheating cost in some economic analyses, primarily because of hydrogen production and delivery costs. Direct electric heating may offer a stronger operating case where low-carbon power is available, but the payback must be modelled against demand charges and grid investment.
For screening purposes, plants often evaluate:
- 1.5–3 years for selected combustion or burner upgrades
- 3–7 years for major electrical or hybrid conversion projects
- Longer or uncertain payback for hydrogen operation without a firm supply contract
These ranges are decision benchmarks, not performance guarantees.
The fuel-switching roadmap
Phase 1: Assessment and technical definition, 0 to 6 weeks
Create a verified fuel and carbon baseline for each furnace. The assessment should include:
- GJ/t and kWh/t by product and operating condition
- Fuel composition and pressure stability
- Furnace-zone temperatures from approximately 900°C to 1,250°C, where applicable
- Burner turndown and operating range
- Stack oxygen, carbon monoxide, and NOₓ
- Refractory materials and hot-face condition
- Gas-train ratings and safety instrumentation
- Electrical connection capacity and available expansion
- Product yield, scale loss, and quality deviations
The output should be a technology-screening matrix, not a generic energy audit, showing which furnace is suitable for hydrogen blending, electric conversion, or staged modernization.
Phase 2: Controlled hydrogen-blend pilot, 6 to 16 weeks
Begin with a limited production campaign and a conservative blend, commonly 5–20% hydrogen by volume, subject to burner and gas-supplier approval.
Track:
- Flame stability and ignition performance
- Furnace-zone temperature deviation
- Steel discharge temperature
- Scale formation and surface quality
- Fuel flow per tonne
- NOₓ and carbon monoxide
- Refractory hot spots
- Burner maintenance requirements
- Safety-system response time
A pilot is successful only when production quality and safety remain stable, not simply when the furnace burns hydrogen.
Phase 3: CAPEX/OPEX modelling, 3 to 6 months
Develop separate business cases for:
- Hydrogen-ready combustion
- Higher hydrogen blending
- Direct electric reheating
- Electric melting
- Oxy-fuel conversion
- Regenerative burner installation
- Gas-electric hybrid operation
The model must include fuel price scenarios, carbon costs, CBAM certificate exposure, oxygen or hydrogen infrastructure, electrical demand charges, downtime during installation, operator training, and spare-component requirements.
The strongest investment case is often the one that preserves optionality. A hydrogen-ready burner package installed today can protect future conversion potential without forcing the plant to purchase hydrogen before supply and pricing become viable.
Phase 4: Full conversion and lifecycle support, 12 to 36 months
Full conversion should proceed only after pilot data, utility capacity, production trials, and financial validation are complete.
The final project should include:
- Approved fuel and electrical architecture
- Updated combustion and safety logic
- Refractory compatibility confirmation
- Operator training and emergency procedures
- Commissioning performance tests
- Carbon-intensity reporting procedures
- Critical furnace spare parts
- Long-term service and response arrangements

Applying the roadmap across furnace applications
The same principles extend beyond a steel rolling mill. Hydrogen-ready and electrically enabled architectures may be evaluated for:
- Heat treatment furnaces serving automotive, aerospace, and defence components
- A melting furnace for steel in foundry and mini-mill operations
- An aluminum melting furnace using recycled feedstock
- A metal recycling furnace processing variable scrap charges
- A hot dip galvanizing plant requiring stable process temperatures
- Thermal processing equipment used in the wire and cable industry
- Continuous casting, CCR, CCM, and steel bar production lines
The fuel strategy must always follow metallurgical requirements. Aluminium melting, steel reheating, annealing, galvanizing, and high-temperature heat treatment do not have identical flame, atmosphere, or temperature demands.
Build the next furnace around flexibility
Continental Furnaces brings more than 35 years of industrial furnace engineering experience to fuel-switching projects. As an established industrial furnace manufacturer, we design customized industrial furnace systems that combine thermal performance, safety, quality control, and lifecycle support.
Our engineers can evaluate hydrogen-ready burners, electric and hybrid thermal architectures, oxygen systems, refractory compatibility, control upgrades, and phased commissioning for new or existing production plants.
Review our furnace spares and accessories gallery or hot dip galvanizing plant solutions, then contact Continental Furnaces to define the correct fuel-switching sequence for your facility.
Do not wait for fuel volatility, CBAM cost, or grid constraints to dictate the project. Consult our engineers now, establish your conversion pathway, and turn decarbonized thermal processing into sustained competitive advantage.