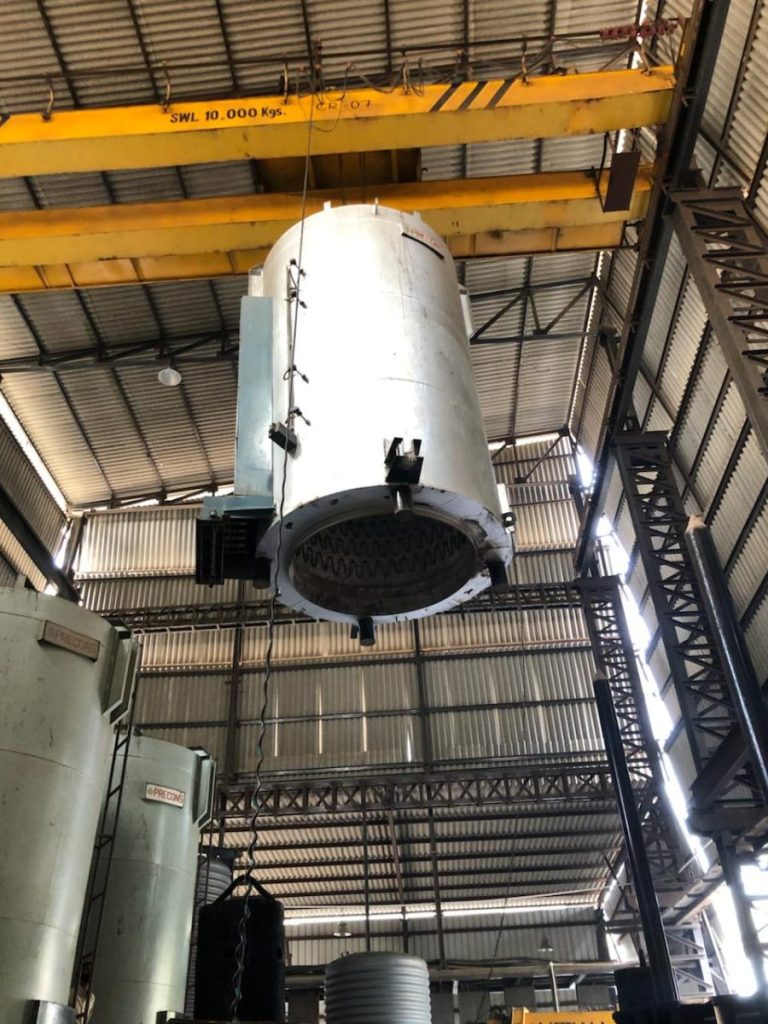
In 2026, refractory and insulation engineering has become one of the most under-rated levers for improving furnace campaign life, production uptime, yield, and energy cost per tonne.
Plant teams often prioritize burners, controls, recuperators, and automation. Those systems are essential, but their performance is compromised when the furnace lining is cracked, chemically attacked, mechanically worn, or thermally inefficient. A deteriorated lining increases shell heat loss, creates temperature non-uniformity, accelerates equipment damage, and drives specific energy consumption upward.
For a steel rolling mill, melting shop, foundry, galvanizing line, or recycling facility, the objective is clear: engineer the refractory and insulation system as a complete thermal asset, not as a periodic repair item.
Why furnace linings fail prematurely
Furnace lining wear is rarely caused by one mechanism. The most severe failures occur when several stressors operate simultaneously:
- Thermal cycling: Repeated heat-up, soaking, cooling, and emergency restart cycles create expansion and contraction stresses.
- Slag and oxide attack: Molten slag, iron oxide, zinc compounds, and other process contaminants penetrate pores and chemically weaken the working face.
- Mechanical abrasion: Scrap charging, billet movement, skids, baskets, charging doors, and cleaning tools can erode refractory surfaces.
- Atmosphere exposure: Oxidizing, reducing, carburizing, or moisture-rich atmospheres alter refractory chemistry and accelerate degradation.
- Local overheating: Poor burner balance, flame impingement, blocked ports, and air infiltration create hot spots.
- Incorrect installation: Poor anchoring, uncontrolled water addition, inadequate curing, and improper dry-out can shorten campaign life before production begins.
The result is a progressive deterioration cycle:
- Cracks and joints open.
- Insulation becomes exposed or compressed.
- Shell temperature rises.
- Fuel or electricity consumption increases.
- Thermal uniformity declines.
- Product quality and campaign reliability suffer.
A modern industrial furnace manufacturer therefore evaluates lining design alongside combustion, loading, controls, and production duty.

The modern refractory and insulation system
A high-performance lining normally combines several engineered layers. Each layer has a distinct function.
1. Working lining: chemical and mechanical protection
The hot face must withstand the highest temperature and the most aggressive process conditions. Depending on the application, suitable materials include:
- High-alumina bricks and castables
- Magnesia-carbon materials for demanding steelmaking zones
- Low-cement and ultra-low-cement castables
- Silicon-carbide-containing castables for abrasion resistance
- Special compositions for zinc, aluminium, slag, and oxide exposure
Low-cement castables provide dense particle packing, high mechanical strength, lower permeability, and improved resistance to crack propagation. They are particularly effective in burner zones, hearths, charging areas, and high-wear sections of melting furnaces.
In a melting furnace for steel, the working lining must be selected against slag chemistry, tapping practice, furnace capacity, and heat frequency. In an aluminum melting furnace or metal recycling furnace, resistance to metal penetration, dross attack, and mechanical charging impact becomes equally important.
2. Intermediate and backup layers: controlled expansion and heat retention
Behind the hot face, the lining system requires structural and insulating layers that manage:
- Thermal expansion
- Anchor movement
- Crack control
- Shell protection
- Heat-flow resistance
- Reduced thermal mass
Ceramic fibre modules are valuable in reheating furnaces, annealing furnaces, and other applications requiring fast heat-up and rapid cycle changes. Their low thermal mass reduces the energy needed to repeatedly heat the furnace structure.
Microporous panels and aerogel-based insulation provide very low thermal conductivity in restricted spaces. They are useful where a plant requires greater insulation performance without increasing overall wall thickness.
These materials must be protected from direct chemical attack and mechanical damage. The correct design is therefore a system of materials, not a single premium product.
3. High-emissivity coatings: improving radiant heat transfer
High-emissivity coatings applied to selected furnace walls, roofs, or refractory surfaces increase radiant heat transfer to the workpiece. When combined with balanced burners and controlled furnace pressure, they can support:
- Lower set-point temperatures
- Shorter soaking periods
- More uniform billet or strip temperatures
- Reduced scale formation
- Lower fuel consumption
High-emissivity coatings do not replace good combustion control or sound insulation. Their value comes from integration with the furnace’s geometry, product loading, atmosphere, and control strategy.
Indicative performance: modern lining versus traditional lining
The following table presents engineering benchmarks for comparable furnace duties. Actual performance depends on furnace size, throughput, product mix, fuel, operating hours, and maintenance quality.
| Performance metric | Traditional firebrick or rammed lining | Modern engineered lining system |
|---|---|---|
| Specific energy consumption | Approx. 1.4–1.8 GJ/t in comparable reheating duty | Approx. 1.2–1.5 GJ/t |
| Shell temperature | Typically 150–220°C in degraded zones | Commonly 90–140°C when correctly designed |
| Campaign life | 12–24 months or frequent local repairs | 18–36 months, with targeted maintenance |
| Thermal uniformity | Greater variation between zones | Improved control and lower hot-spot risk |
| Installation downtime | 10–20 days for extensive replacement | 5–14 days for engineered modular or castable repair |
| Energy penalty over campaign | Often rises progressively as lining degrades | More stable across the campaign |
| Indicative ROI period | Not applicable | Approximately 12–36 months |
Well-designed refractory upgrades can deliver 8–18% lower furnace energy consumption, while advanced insulation and monitoring can prevent the gradual 15–25% increase in specific energy consumption often associated with undetected lining deterioration.
Campaign life improvements of 30–50% are achievable in aggressive services when material selection, installation quality, operating discipline, and inspection are addressed together.
Where the gains apply across industrial furnace systems
The same engineering principles transfer across multiple applications:
- Steel rolling mill: Reheating furnaces, soaking pits, walking-beam furnaces, and equalizing furnaces benefit from reduced shell loss and more stable billet temperatures.
- Heat treatment furnaces: Ceramic fibre modules and low-mass linings reduce cycling energy while supporting accurate temperature profiles.
- Melting furnace for steel: High-performance hot-face materials resist slag, thermal shock, and charging impact.
- Aluminum melting furnace: Dense, chemically compatible linings limit metal penetration and dross-related degradation.
- Hot dip galvanizing plant: Annealing furnaces, zinc-pot zones, and associated thermal equipment require resistance to heat, atmosphere, and process contamination.
- Wire and cable industry: Continuous annealing and galvanizing lines require stable thermal profiles, low leakage, and fast-response insulation.
- Metal recycling furnace: The lining must tolerate variable scrap chemistry, irregular charging, abrasion, and frequent thermal cycling.
Continental Furnaces’ heat treatment furnace solutions and melting and recycling projects demonstrate how thermal processing equipment can be configured around the customer’s material, throughput, and operating conditions.
Refractory engineering and the 2026 steel transition
The move toward higher EAF production, scrap-fed melting, DRI-based steelmaking, and green steel targets is changing refractory requirements.
Modern steel plants must prepare for:
- Higher scrap ratios and more variable input chemistry
- Increased EAF share and more frequent thermal cycling
- DRI and hot-briquetted iron charging
- Higher electrical loads and demand for flexible production
- Decarbonisation reporting based on energy per tonne
- Compatibility with waste heat recovery and hybrid heating
- Digital monitoring of shell temperature and lining condition
The International Energy Agency’s iron and steel analysis identifies scrap use, electrification, hydrogen-based production, and energy efficiency as central decarbonisation pathways. Refractory engineering supports each pathway by stabilizing heat transfer and reducing avoidable energy loss.
A well-insulated furnace is also more compatible with waste heat recovery. Lower uncontrolled wall losses allow more of the remaining thermal energy to be directed toward combustion-air preheating, charge preheating, or other plant heat sinks.
A four-phase roadmap for lining performance
Phase 1: Assessment and thermography
Begin with a verified baseline before selecting materials.
Measure and document:
- Specific energy consumption in GJ/t, kWh/t, or fuel per tonne
- Shell temperature across all accessible surfaces
- Furnace pressure and air infiltration
- Burner balance and flame pattern
- Lining thickness, age, and repair history
- Product temperature uniformity
- Campaign life and unplanned downtime
- Flue-gas temperature and oxygen concentration
Infrared thermography should be performed during stable production and repeated at defined intervals. A growing hot spot is an early warning of insulation collapse, anchor failure, joint opening, or hot-face erosion.
Phase 2: Material selection and design
Select the lining by zone, not by furnace average.
The design review should cover:
- Hot-face chemistry and wear mechanism
- Low-cement castable formulation
- Ceramic fibre or insulating brick thickness
- Microporous or aerogel backup insulation
- Expansion joints and anchor layout
- Burner and flame-impingement zones
- Door surrounds, hearths, skids, and charging areas
- High-emissivity coating compatibility
- Dry-out and commissioning requirements
This phase converts operating data into a documented thermal design with measurable performance targets.
Phase 3: Installation and dry-out
Installation quality determines whether the specified material achieves its rated performance.
Control:
- Substrate preparation
- Anchoring and joint placement
- Castable water content
- Vibration and compaction
- Module compression
- Curing time
- Controlled dry-out temperature ramps
- Moisture removal and furnace ventilation
A rushed dry-out can create steam pressure, explosive spalling, and premature cracking. Planned downtime is less expensive than an avoidable refractory failure during production.
Phase 4: Monitoring and lifecycle management
Campaign management should continue after commissioning.
Establish a dashboard linking:
- Shell thermography
- Energy per tonne
- Furnace-zone temperatures
- Burner status
- Product discharge temperature
- Repair locations
- Campaign heats or operating hours
- Downtime events
- Refractory and furnace spare parts consumption
Industry 4.0 monitoring converts refractory maintenance from reactive repair to predictive lifecycle management. It also creates an auditable record for energy management and regulatory compliance.

Build the business case around total lifecycle value
The lowest initial lining cost is not the lowest-cost solution. Procurement teams should evaluate:
- Energy cost per tonne
- Production lost during repair
- Campaign extension
- Reduced emergency maintenance
- Lower shell-temperature risk
- Improved product yield
- Compatibility with future fuels and controls
- Availability of replacement materials and spare parts
- Supplier response time
The strongest return often comes from a combined project covering refractory, insulation, burner tuning, sealing, thermography, and controls. This approach creates a quantum leap in lifecycle value rather than a narrow repair benefit.
Continental Furnaces: an enduring engineering partnership
Continental Furnaces brings 35+ years of experience to the design and manufacture of customized thermal processing solutions. Our approach combines energy-efficient technology, ISO-certified quality, application-specific engineering, and prompt lifecycle support.
As an experienced industrial furnace manufacturer, we support steel, foundry, galvanizing, recycling, automotive, aerospace, construction, and the wire and cable industry with complete industrial furnace systems and responsive technical service.
For a plant-specific assessment, explore our energy-efficiency guidance, review consulting support, or contact Continental Furnaces.
Conclusion: engineer the lining for sustained competitive advantage
Refractory and insulation engineering directly influences campaign life, fuel consumption, temperature uniformity, maintenance cost, and production reliability.
The 2026 action plan is decisive:
- Thermographically map the current condition
- Benchmark energy per tonne
- Match materials to each wear mechanism
- Reduce shell heat loss
- Integrate monitoring with maintenance
- Protect future compatibility with scrap, DRI, EAF, hydrogen, and waste heat recovery
- Manage the lining as a lifecycle asset
Do not wait for a visible failure before addressing thermal losses. Invite Continental Furnaces to assess your lining architecture, operating data, and campaign objectives. A structured refractory and insulation programme is an essential strategic move toward lower specific energy consumption, higher uptime, and sustained competitive advantage.